Membrane Bioreactor (MBR)

Turning wastewater into high-quality effluent.

Product Description

The membrane bioreactor (MBR) has emerged as an efficient compact technology for municipal and industrial wastewater treatment. Compared to traditional methods such as activated sludge and oxidation ditches, MBR offers the advantage of eliminating secondary sedimentation tanks and other process steps, significantly reducing the footprint while producing stable, high-quality permeate. Built on hollow fiber PVDF as the internal support, Suntar MBR membrane modules have a tensile strength of over 200 N, so they withstand repeated air scouring.

Download Brochure

Please click and fill a simple form to enable the brochure download.

Learn More

Need more information or a quote? Our team is ready to help.

What Is a Membrane Bioreactor (MBR)?

Turning wastewater into high-quality effluent, MBR technology delivers sustainable solutions for cleaner water management.

A Membrane Bioreactor (MBR) is a wastewater treatment process that integrates a biological treatment unit such as activated sludge with a membrane filtration unit (typically microfiltration or ultrafiltration) to separate solids from liquids. This technology allows for efficient wastewater treatment while producing high-quality effluent. In the MBR process, membranes serve as a solid-liquid separation device, retaining the biomass within the bioreactor before discharging the treated effluent into the environment. Suntar supplies MBR wastewater treatment systems in two formats, Graphene MBR and Bundle MBR.

Applications of MBR

MBR is used in municipal wastewater treatment for domestic and municipal sewage, in industrial wastewater treatment for the food and beverage, biopharmaceutical, textile and chemical industries, and in water reuse for non-potable applications.

Technical Features of MBR

Key Benefits of MBR

Product Portfolio

Suntar offers two MBR membrane formats, both built on our hollow fiber PVDF technology.

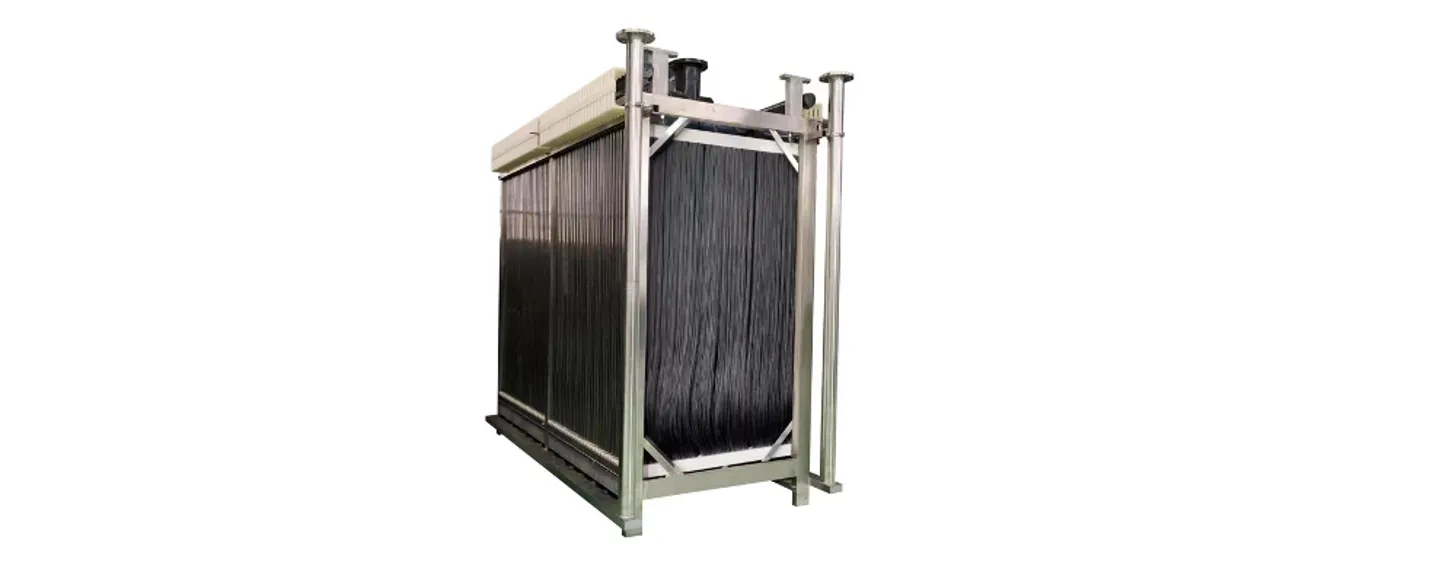
Suntar Graphene MBR module with black membrane fibres in a stainless steel frame

Graphene MBR

Graphene Hollow Fiber Membranes operate in open-air tanks, ideal for high suspended solids. They withstand fluctuations, offer customisable membrane areas, and outperform pressurised ultrafiltration in resilience. Containerised setups provide added flexibility.

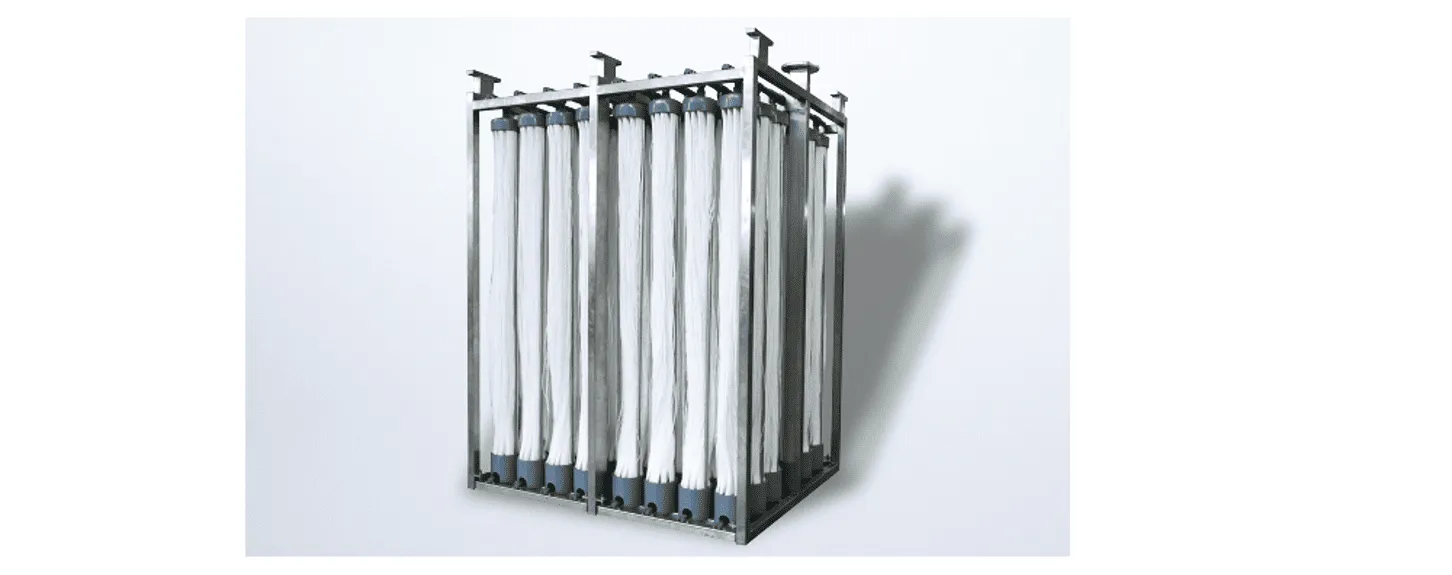
Suntar Bundle MBR module with white membrane fibre bundles in a stainless steel frame

Bundle MBR

The Bundle Membrane Bioreactor is ideal for small-scale, decentralised treatment. This modular system offers flexible capacity, supports various cleaning methods, and has a single-end outlet designed to handle higher pressure drops efficiently.

Most Frequently Asked Questions

What types of membranes are used in MBRs?

Microfiltration (MF): Used for separating larger particles and suspended solids.

Ultrafiltration (UF): Typically used for finer filtration, capturing smaller particles and bacteria

  • Regular maintenance and cleaning of membranes to reduce fouling.
  • Monitoring and adjusting aeration rates to ensure proper biomass growth.
  • Using appropriate chemicals for cleaning and maintaining membrane performance.
  • Implementing advanced control systems for better monitoring and optimization of the process.

Related Industries

From water treatment to process separation, discover how our innovative solutions drive sustainable performance across the global industries.

Data Centre Water Solutions

The Path to Net-Zero WUE

Biopharmaceuticals

Industrial Water and Wastewater Treatment

Suntar provides industrial water and wastewater treatment systems for 12 industries, from power plants to oilfields, integrating proprietary membrane technologies developed and manufactured at our own production facilities. For sewage and town water, see our municipal wastewater treatment solutions.

Interested in learning more about what we do at Suntar?

We conduct various webinars on our solutions from time to time.

Download Brochure

Please provide us with your details to receive brochure.